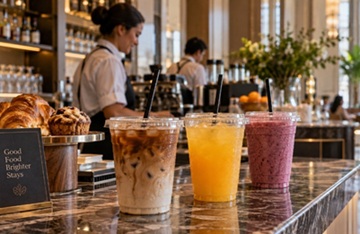
 INTERNATIONAL REPORT—Cold drink cups rarely attract much attention in hotel procurement until a property decides to change them.
Then what looked like a simple sustainability decision becomes an operating question. Breakfast juice, iced coffee, smoothies, conference drinks and poolside beverages may all be cold, but they do not behave the same way in service. A change in cup material can also mean new lids, new storage requirements, different printing behavior and, in some cases, a completely different waste route.
The result is that hotels are not really choosing a cup. They are choosing a small beverage-packaging system. That system needs to work for the drink, the outlet, hotel staff, guests and the waste infrastructure available after use.
Start with the Service Environment, Not the Material
A full-service hotel can easily have four or five different cold-drink environments within the same property.
Breakfast may serve juice and iced coffee. A lobby café may add cold brew, matcha and smoothies. Conference catering may require hundreds of identical cups within a short service window. A fitness area may offer protein drinks, while a pool bar introduces heat, condensation and wet-hand handling.
Green Lodging News has already documented how this kind of outlet mix is becoming part of modern hospitality. At 1 Hotel Tokyo, for example, the Neighbors Café combines grab-and-go food with artisan coffee and tea, illustrating how beverage service increasingly sits somewhere between restaurant, café and takeaway.
The packaging decision should therefore begin with the service conditions rather than with a material preference.
| Hotel Application | Main Packaging Pressure | What Buyers Should Test |
| Breakfast juice | Fast service, simple lid, high volume | Working capacity, lid speed, stackability |
| Iced coffee / lobby café | Ice, branding, takeaway handling | Lid retention, condensation, print contrast |
| Smoothies | Thick product, toppings, dome clearance | Headspace, lid geometry, straw access |
| Conference catering | High SKU volume, rapid setup | Shared lid systems, storage, carton efficiency |
| Poolside service | Heat, wet hands, outdoor use | Grip, condensation, lid security |
| Grab-and-go | Carry distance, branding, waste route | Carrier fit, labeling, disposal instructions |
This table is more useful to a hotel buyer than a simple comparison of PET versus PLA because it begins with how the cup will be used.
Capacity Should be Tested with the Finished Drink
Nominal capacity is not the same as working capacity. A 16 oz menu drink does not necessarily belong in a cup whose practical fill limit is exactly 16 oz. Ice, foam, fruit and toppings consume space, and staff still need enough headroom to apply the lid quickly without spilling the drink.
For that reason, sample approval should involve the actual beverage. Fill the cup exactly as staff would during normal service, add the usual ice and toppings, close the intended lid and leave the drink for the expected holding time.
That test quickly exposes issues that catalogue specifications do not show: insufficient headspace, poor grip after condensation, unstable lids and cups that do not fit existing carriers or dispensers.
For a hotel chain, these apparently minor issues scale rapidly. A cup that slows service by only a few seconds can become noticeable during a breakfast rush or conference break.
The Biggest SKU Problem is Often the Lid System
Hotels tend to compare cup prices, but the operational complexity often sits above the rim.
If every cup size introduces a different lid family, the property needs more storage, more inventory records and more staff training. The risk of selecting the wrong lid also rises during high-volume service.
A better approach is to build the cup range around a deliberate rim architecture. For example, selected PLA cup families are available with 98 mm rims across several capacities. In the currently published Bioleader Cups range, selected 12 oz, 16 oz and 24 oz PLA variants are available with a 98 mm rim:
| Selected Cup Variant | Published Capacity | Rim |
| 12 oz PLA | 400 ml | 98 mm |
| 16 oz PLA | 500 ml | 98 mm |
| 24 oz PLA | 680 ml | 98 mm |
That creates the possibility of a 98 mm unified rim system across several core beverage sizes. The operational objective is straightforward: reduce the number of lid families while retaining enough cup sizes to cover the menu.
But there is an important qualification. The same nominal rim diameter does not automatically prove that every cup uses the same lid.
Cup profile, rim bead geometry, lid construction and supplier tooling still need to be validated for the exact SKUs. A 98 mm strategy should therefore be treated as a shared-rim shortlist, followed by actual cup-and-lid approval—not as permission to mix any products that happen to carry “98 mm” in the catalogue. Cupschina’s own sourcing guidance makes the same distinction.
For hotel procurement, this is what a real industrial solution looks like: not “buy fewer lids” as a vague recommendation, but select a core rim family, shortlist the exact cup SKUs, then physically qualify one flat, dome or sip lid series against those exact cups.
Reusable, PET and PLA Belong to Different Operating Systems
A hotel should not assume there is one universally sustainable cold-cup material.
Green Lodging News recently reported a new Eco-Products beverage range that deliberately included compostable, recyclable and reusable options side by side. The company’s own explanation was telling: no single solution works everywhere because waste infrastructure and service models differ.
A practical hotel comparison looks more like this:
| Option | Where it Can Make Sense | Main Procurement Question |
| Reusable cup | Closed systems such as pool areas, staff cafés or controlled outlets | Can the hotel collect, wash and return it reliably? |
| PET cold cup | Clear beverage presentation where recycling infrastructure accepts PET | Will the local recycling system actually accept the finished cup? |
| PLA compostable cup | Cold-drink programs linked to commercial compost collection | Is the finished cup certified, and will the composter accept it? |
PET is commonly identified as Resin Identification Code #1, but that code identifies the resin; it is not, by itself, proof that a specific cup will be recycled locally. ASTM’s Resin Identification Code standard explicitly separates resin identification from a recyclability claim.
That distinction is particularly important for hotels, where guests may read a number or recycling-style symbol as an instruction even when the local recovery system does not accept the product.
Compostable Cups Need Both a Standard & a Waste Route
For PLA cups, “compostable” should be tied to a defined standard rather than used as a broad environmental description.
In Europe, EN 13432 is widely used for packaging intended for industrial composting. In North America, the current active version of ASTM D6400 is ASTM D6400-26, covering plastics and products designed for aerobic municipal or industrial composting facilities. ASTM updated D6400 in 2026, and BPI uses ASTM D6400 as the base standard for its Commercial Compostability Certification Program.
BPI is a third-party certification organization, not a regulator. Its certification gives buyers an independent way to verify that a listed product meets the applicable ASTM compostability requirements; its public product database can also be used to confirm individual certified items.
Certification, however, only answers the technical question. The hotel still has to answer the operational one. Does the property collect compostables separately? Does the waste hauler accept serviceware? Does the commercial composter accept that exact category of product?
The EPA’s foodservice guidance is explicit on this point: commercially compostable serviceware makes sense where an appropriate composting program exists, accepts the products and is supported by proper collection.
A certified cup that goes into mixed trash remains a certified cup, but it does not achieve the end-of-life outcome the hotel may be communicating to guests.
Condensation Belongs in the Specification
Cold cups should also be approved wet, not just empty. Condensation changes how the cup feels, how labels adhere and how guests handle it. This becomes especially noticeable on pool decks, outdoor terraces and in humid climates. A realistic approval process should fill the cup with the intended drink and ice, then review it after ten to fifteen minutes in the actual service environment. Procurement teams should check grip, lid retention, carrier fit, print appearance and whether external moisture creates problems for labels or adjacent paper packaging.
This does not require a laboratory. It requires testing the package under conditions that resemble actual service. For hotels, that is often more valuable than another generic material data sheet.
Transparent Cups Need Real Prepress Engineering
Custom printing on a clear cup is another area where hotels can move from basic artwork approval to a more technical specification. The drink itself becomes part of the visual background. A white hotel logo may look clean on an empty cup and disappear over lemonade or pale milk tea. The same artwork may look much stronger over cold brew.
Where the selected printing process supports it, a spot-white underprint can be used beneath selected artwork to improve opacity and contrast. That white layer should be treated as part of the print construction, however, because poor registration between the white base and upper colors can leave a visible halo or edge. Cupschina’s current prepress guidance specifically recommends evaluating white underprint against the final beverage rather than assuming that a digital proof will predict the result.
Tapered cups create a second issue. Artwork designed as a flat rectangle does not simply wrap onto a conical cup without distortion. Production files should be prepared using the exact cup’s curved or fan-shaped print template, so the artwork is geometrically compensated before printing. This is sometimes described as arc distortion compensation.
One common mistake is to apply universal “safe area” numbers to every cup. That should be avoided. There is no single industry rule saying that every clear cup requires exactly 15 to 20 mm of clearance from the rim and 10 to 15 mm from the bottom. Printable boundaries depend on cup geometry, taper, machine setup and printing process. Buyers should require the supplier’s SKU-specific production template and verified print area instead.
For a hotel brand, that is a much stronger production requirement than simply telling a designer to “keep the logo away from the edges.”
QR Codes Should be Qualified on the Filled Cup
The same principle applies to QR codes used for loyalty programs, digital menus, events or guest offers. The code is printed onto a curved transparent surface, while the beverage behind it can change the contrast. Condensation adds another variable.
A QR code should therefore be tested on the actual printed cup under realistic fill conditions. Where required, a continuous light or white backing panel can stabilize contrast behind both the code and its required quiet zone. The production sample—not the PDF—is the final approval reference. That is especially relevant for hotels that use one branded cup across several drinks with very different colors.
Bioleader Cups as a System Example
Hotels reviewing cold-drink packaging can use suppliers such as Bioleader Cups as a reference for how a multi-size cup program can be structured around PET and PLA materials, multiple rim families, matching flat, dome and sip lids, and custom printing.
The relevant value is not the number of products in the catalogue. It is whether the supplier can help reduce the system to the fewest practical combinations. For example, if a property’s core menu can be served with selected 12 oz, 16 oz and 24 oz cups in a qualified 98 mm rim family, the purchasing conversation can move away from three unrelated cup-and-lid combinations toward a controlled shared-rim architecture.
That should still be validated with the exact lid and exact cup SKU.
Standardization should remove unnecessary complexity, not remove functions the beverage actually needs.
What Hotel Procurement Should Approve Before Rollout
A practical approval matrix can remain short:
| Item | Minimum Approval Question |
| Drink application | Has the cup been tested with the real beverage, ice and toppings? |
| Capacity | Is working volume sufficient, not just nominal ounces? |
| Rim system | Can core sizes share one qualified lid family? |
| Lid | Has the exact lid been physically tested on the exact cup? |
| Material | Does PET, PLA or reuse fit the property’s actual recovery route? |
| Compostability | Is the finished product supported by EN 13432/ASTM D6400 or relevant third-party certification? |
| Printing | Has the artwork been built on the exact cup template? |
| White underprint | Is it needed for contrast over real beverage colors? |
| Condensation | Has the filled cup passed a wet-cup handling test? |
| Waste route | Has the local recycler or composter confirmed acceptance? |
This is the level at which a cold-cup change becomes manageable for procurement.
Let Staff Test the System Before the Guest Does
The final approval should happen in service, not in a meeting room. Give the samples to breakfast staff, baristas, banquet teams and pool attendants. Ask them to prepare the normal drinks, use the real lids and handle the cups through a typical service period.
They will quickly identify problems that do not appear on a specification sheet: a lid that takes too much force to apply, two cup sizes that look almost identical, a dome lid that consumes too much shelf space, or a cup that no longer fits the dispenser.
That trial is also the right time to test condensation, printed branding and disposal instructions. The objective is not to find one perfect cold cup for the entire hotel industry. It is to create a cup system that the property can operate. The cup must fit the drink. The lid must fit the cup. The material must fit the waste route. And the number of SKUs must fit the people who will manage them every day.
When those four things align, the sustainability claim becomes much easier to defend—and the packaging becomes much easier to live with.